Buying China Fasteners can look simple until a shipment arrives with mixed grades, uneven plating, or threads that resist assembly. Product photos rarely reveal these risks. The real work begins with specifications, supplier verification, sampling, and clear quality expectations.
This guide presents ten practical tips for purchasing reliable fasteners from China. It considers material grades, dimensions, thread standards, coatings, packaging, inspection, and documentation. Standards such as ISO, ASTM, and DIN can provide useful reference points, but they must match your application and local requirements. A professional supplier should explain tolerances clearly and provide consistent test reports. Details matter.
Experience shows that the lowest quotation is not always the lowest total cost. Delayed production, rejected parts, and emergency replacements can quickly change the calculation. Buyers should compare samples, production capacity, communication quality, and traceability before placing a large order. Ask who controls the steel, who checks the threads, and how defects are handled. Small errors compound.
Some recommendations may require adjustment. A small workshop may offer excellent craftsmanship, while a large factory may provide stronger process control. Neither assumption is enough. Your decision should depend on evidence, risk level, order volume, and required certification. A careful purchasing process protects performance and budget without making unrealistic promises. These ten tips are designed to support practical, documented, and dependable sourcing decisions.
When buying China fasteners, define the required ISO 898-1 property class before discussing price. Grade 8.8 provides a nominal tensile strength of 800 MPa and a yield strength near 640 MPa. Grade 10.9 reaches approximately 1,000 MPa tensile strength and 900 MPa yield strength. These values guide joint design, preload, and safety margins.
Do not select 10.9 simply because it is stronger. Higher strength can increase sensitivity to hydrogen embrittlement, thread damage, and incorrect tightening. Check the bolt diameter, thread pitch, length, head marking, surface treatment, and service temperature. Confirm whether the joint needs controlled preload or frequent disassembly. A torque chart alone is not enough, because lubrication changes the torque-tension relationship.
I once focused on the grade and overlooked the coating thickness. That shortcut was wrong. The extra coating affected thread engagement during assembly. Ask the supplier for material certificates, dimensional inspection records, hardness results, and tensile test reports from the same production lot. Independent testing can verify the claims before shipment. Inspect sample markings and packaging when the fasteners arrive. Keep the purchase specification precise, including ISO 898-1 grade, thread tolerance, coating, inspection method, and acceptance limits. Small wording gaps create expensive arguments later.
10 Tips for Buying China Fasteners
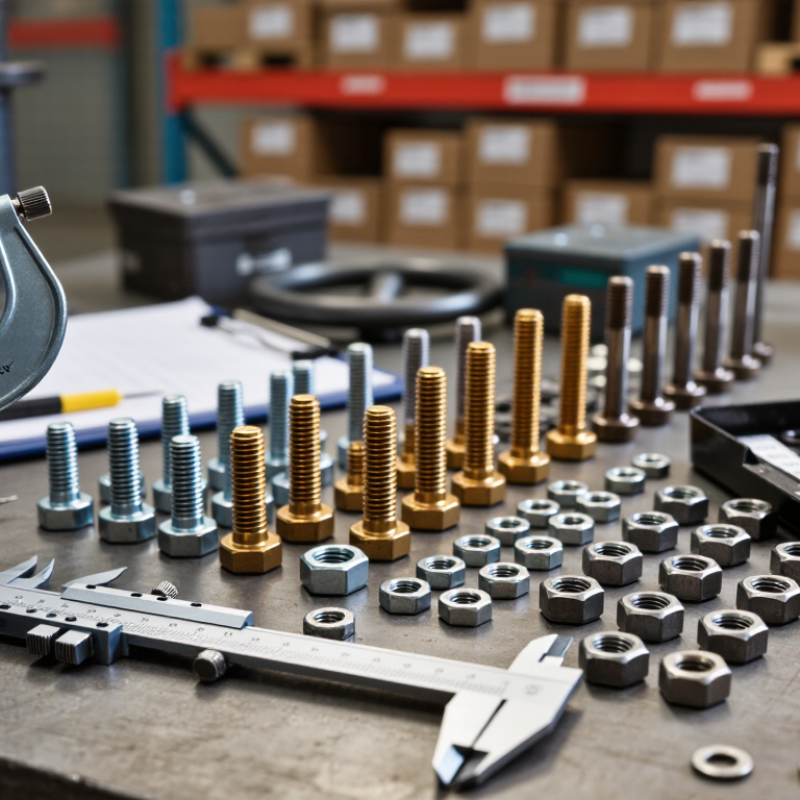
A reliable purchase begins with a controlled drawing, not a supplier photograph. For hexagon head bolts, compare the offered part with ISO 4014 requirements. Check nominal diameter, length, head height, across-flats size, and the unthreaded shank length. Measure several pieces with calibrated calipers. One sample can look perfect and still hide variation.
Tip: Confirm the thread before discussing price. ISO 965 defines metric thread tolerances and helps establish whether the bolt and nut will fit correctly. Record the thread diameter, pitch, tolerance class, and fit requirement. A 10 mm bolt with the wrong pitch is not a small error. It may stop assembly completely. Use a calibrated thread gauge or matching nut, then verify critical batches with suitable gauges. Ask for inspection records, material information, and dimensional reports tied to the actual lot. Generic certificates are weak evidence.
Tip: Define acceptance limits in writing. ISO 4014 does not replace your engineering drawing or application requirements. Specify coating thickness, surface condition, mechanical property class, and sampling rules separately. Inspect packaging labels and lot numbers when goods arrive. I have seen buyers focus on head markings while missing a short threaded length. That mistake is easy to repeat. No inspection plan is perfect. Review failed samples honestly, adjust the drawing, and improve the next order.
| Tip | What to Verify | Practical Inspection Method | Reference Data or Example | Recommended Acceptance Evidence | Applicable Standard |
|---|---|---|---|---|---|
| 1 | Confirm the fastener type and thread coverage. | Check that the bolt has a hexagon head and a partially threaded shank. Measure the threaded length and compare it with the approved drawing. | An ISO 4014 bolt is a hexagon head bolt with a metric thread and a short unthreaded shank section. It is not interchangeable with a fully threaded screw unless specified. | Approved drawing, dimensional report, and sample measurement agree. | ISO 4014 |
| 2 | Verify nominal diameter and length. | Measure the major diameter with a calibrated micrometer or thread measuring instrument. Measure bolt length from the bearing surface under the head to the end of the bolt. | For an M10 × 50 bolt, the nominal diameter is 10 mm and the nominal length is 50 mm. The head is not included in the nominal length. | Measured dimensions remain within the drawing and applicable product-standard limits. | ISO 4014; purchaser’s drawing |
| 3 | Check the thread designation and pitch. | Use a metric thread pitch gauge or calibrated optical measurement equipment. Confirm the pitch shown on packaging, drawings, and inspection reports. | Typical coarse-pitch examples are: M6 × 1.0, M8 × 1.25, M10 × 1.5, M12 × 1.75, M16 × 2.0, and M20 × 2.5. | The actual pitch matches the ordered designation; fine-pitch variants are not substituted without written approval. | ISO 261; ISO 965 |
| 4 | Specify the external thread tolerance class. | Require the supplier to state the tolerance class on the drawing or inspection report. Verify with calibrated GO/NO-GO thread gauges or an equivalent validated method. | 6g is a commonly used external metric thread tolerance class for general-purpose fastening applications. The tolerance class must be agreed before production. | Gauge results and the inspection report identify the required external tolerance class. | ISO 965-1; ISO 965-2 |
| 5 | Match the bolt thread with the mating internal thread. | Test the bolt with a verified mating nut or calibrated internal thread gauge. Check full engagement without binding, cross-threading, or excessive looseness. | A common matched combination is an external 6g thread with an internal 6H thread, subject to the application and engineering specification. | The assembled thread runs smoothly by hand for the specified engagement length. | ISO 965-1; ISO 965-2 |
| 6 | Verify head dimensions and tool fit. | Measure head height, width across flats, and bearing-surface geometry. Test the correct wrench or socket on production samples. | Head dimensions must correspond to the ordered nominal diameter and product grade. Do not assume that a visually similar head has the correct across-flats dimension. | Head dimensions meet the approved product table, and the specified tool seats fully without rocking. | ISO 4014; applicable dimensional tables |
| 7 | Check the unthreaded shank and thread runout. | Measure the plain shank diameter, unthreaded length, and transition area. Inspect for incomplete threads, folds, laps, or damaged thread runout. | The plain shank should provide the specified fit in the joint. Thread runout must not prevent the bearing surfaces from seating correctly. | No visible thread defects interfere with installation, clamping, or joint alignment. | ISO 4014; approved drawing |
| 8 | Validate material, property class, and markings. | Review the material certificate and perform hardness, tensile, or other required mechanical tests. Confirm head markings where required by the specification. | Common carbon-steel property classes include 8.8 and 10.9, but the correct class depends on the engineering design. Property class is not the same as thread tolerance class. | The test report confirms the ordered property class and required mechanical properties. | ISO 898-1; purchase specification |
| 9 | Inspect surface finish and corrosion protection. | Check the agreed coating or finish, coating coverage, visible damage, and signs of corrosion. If required, perform coating thickness or corrosion-resistance testing. | Examples include plain steel, zinc coatings, or other specified finishes. Coating requirements should state the system, thickness, appearance, and test method. | The finish matches the approved sample and purchase specification without peeling, bare areas, or red rust. | ISO 4042 or specified coating standard |
| 10 | Require batch traceability and final sampling. | Ask for lot identification, quantity, production date, inspection records, and retained samples. Use a documented sampling plan before shipment. | Inspection should cover dimensions, thread gauges, visual condition, markings, mechanical properties, and coating requirements as applicable to the order. | Each shipment can be traced to a production lot and has a signed final inspection report. | ISO 2859-1; ISO 3269; purchase specification |
Note: ISO 4014 defines dimensional requirements for hexagon head bolts with metric coarse and fine pitch threads, while ISO 965 defines the general system of limits and fits for ISO metric screw threads. The purchaser’s drawing and agreed inspection specification should take precedence where application-specific requirements are stricter.
When buying stainless-steel fasteners from China, compare the ISO 3506 grade before comparing prices. A2 is commonly associated with 304-type stainless steel and suits indoor, dry, or mildly humid applications. A4 is commonly compared with 316-type stainless steel and offers better resistance to salt and chlorides. Neither grade is completely corrosion-proof.
Tip 1: Match the material to the location. A2 may work inside a clean workshop, but A4 is usually safer near coastlines, swimming pools, and chemical exposure.
Tip 2: Check the full marking, such as A2-70 or A4-80. The number indicates the tensile-strength class, not corrosion performance. A4-80 is stronger than A4-70, but strength still depends on the application and thread design.
Ask the supplier for lot-specific inspection reports, chemical composition results, and mechanical test data. Verify that markings on the head match the documents. A digital caliper can confirm dimensions, but it cannot prove stainless-steel grade. Request traceability from raw material to finished batch. Salt-spray results can help, yet they should not replace ISO documentation or real environmental analysis.
Tip 3: Inspect sample threads under bright light. Rough threads, dark stains, or inconsistent passivation deserve questions.
Tip 4: Specify surface treatment clearly. I would not rely on “stainless steel” alone; that wording is too vague. A small mistake in grade selection can become expensive after installation, especially when chloride exposure was underestimated.
10 Tips for Buying China Fasteners: Audit Suppliers Through ISO 9001, Mill Certificates, and Lot Traceability
ISO 9001 is a useful starting point, not a guarantee of fastener quality. The ISO Survey 2022 recorded 1,265,216 ISO 9001 certificates worldwide. That large figure shows adoption, but it does not confirm product conformity. Ask for the certificate’s scope, factory address, expiry date, and latest audit status. The scope should cover fastener manufacturing, not only trading or distribution. Then compare the certificate details with the actual production site. Small mismatches matter.
Request a mill certificate for every relevant material lot. Check the heat number, chemical composition, tensile results, hardness, standard, and test method. For metric bolts, verify that the reported properties match the specified property class under ISO 898-1. A certificate without heat identification is weak evidence. It is only paperwork. Trace one carton backward to the raw-material heat, production traveler, inspection record, and final release report. Then trace the same lot forward to the shipping documents. This practical test often exposes gaps. I have found that suppliers may maintain excellent records but still mix labels during repacking. That risk deserves attention. Use sampling plans based on ISO 2859-1, and record nonconformities instead of accepting verbal explanations. Perfect audits are unlikely; repeated unexplained gaps are unacceptable.
How to use this chart: Compare the minimum tensile strength stated on the mill certificate with the selected ISO 898-1 property class. An ISO 9001 certificate confirms the supplier's quality-management system, but it does not replace product testing. Confirm that each mill certificate identifies the material grade, heat number, test results, and lot information that can be traced to the delivered fasteners.
10 Tips for Buying China Fasteners?
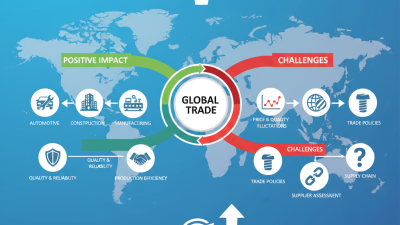
Control coatings, testing, packaging, and landed cost before ordering. A low unit price can hide expensive rework. The World Bank’s 2023 Logistics Performance Index gave China an overall score of 3.7 out of 5, but shipment performance still varies by port and season. Request a written quotation with steel grade, dimensions, tolerance, coating system, packaging, delivery term, and validity period. Confirm whether prices include tooling and inspection fees. My early mistake was comparing carton prices only. Freight changed the decision.
Define the coating before production. Specify zinc thickness, passivation, topcoat, friction requirements, and corrosion test method. Do not treat salt-spray hours as real service life. The NACE IMPACT study estimated global corrosion costs at 3.4% of worldwide GDP, while proper prevention could save 15–35%. Ask for coating certificates and verify samples through an independent ISO/IEC 17025 laboratory. Test hardness, tensile strength, proof load, thread gauges, dimensions, and surface defects. Keep heat numbers and batch records linked to inspection results. Small gaps here become large claims later.
Packaging needs equal attention. Use separate, labeled lots, moisture barriers, desiccants, edge protection, and readable carton marks. Photograph loading conditions. UNCTAD’s Review of Maritime Transport reports that shipping carries over 80% of global merchandise trade by volume, so transit exposure matters. Calculate landed cost, including ocean freight, insurance, duties, customs handling, inland delivery, testing, inventory financing, and rejected parts. Add a realistic contingency. Not every risk fits neatly in a spreadsheet. Supplier audits, pre-shipment inspection, and a pilot order can reveal problems before a full container is committed.