Choosing the right Rivets can make the difference between a dependable joint and one that loosens under vibration. The choice is not just about diameter or appearance. Material, head style, grip range, joint thickness, and access to the back of the workpiece all matter. A small aluminum panel, for example, may call for a different rivet than a steel bracket exposed to moisture.
Start by identifying the materials being joined and the conditions they will face. Match the rivet’s grip range to the combined thickness of the pieces, and check the manufacturer’s strength and installation guidance. If the joint will carry repeated or heavy loads, do not rely on appearance alone. The right-looking fastener can still be wrong. Tool compatibility matters, too: a blind rivet can be installed from one side, while other designs may require access to both sides. That detail matters.
This guide explains how to compare common rivet types, materials, sizes, and head styles, then narrow the options for a particular project. It also covers practical checks, such as making a test joint with scrap material and inspecting the finished set for movement or gaps. Those checks are easy to skip when a job seems simple. They are not a substitute for engineering advice when failure could cause harm, and product specifications should take priority over guesswork. Even experienced builders can overlook a detail. A careful choice begins with the joint itself, not the fastener display.
Before choosing a rivet, sketch the joint and mark the direction of each expected force. A lap joint pulled sideways mainly loads the rivet in shear. A panel being pulled away from its support places more demand on tensile strength. Direction matters. Some assemblies experience both loads, especially near vibrating equipment or flexible panels.
Compare the required load with published shear and tensile ratings for the exact rivet size and material. Ratings may depend on the rivet body, mandrel, sheet thickness, and test method. Do not treat a shear rating as a tensile rating. For example, a thin aluminum panel may tear around the hole before a strong steel rivet reaches its stated capacity. The surrounding material matters too.
Check the rating conditions against your real joint, including grip range, hole diameter, and material combination. Then allow a suitable margin for uneven load sharing, installation variation, and repeated stress. A single average load can hide a sharp peak at one fastener. That detail is easy to miss. If loads combine or failure could cause injury, have the joint reviewed and tested by a qualified engineer; published ratings alone cannot predict every field condition.
A rivet standard helps you compare more than head shape. It can define dimensions, tolerances, and performance requirements. For solid rivets, ASTM B18.1.1 covers small solid rivets; ASTM B18.1.2 covers large ones. For open-end blind rivets with a protruding head, ISO 15977 addresses aluminum rivets with aluminum mandrels. Check the exact standard edition and product scope before ordering. Similar-looking rivets may not meet the same requirements.
Match the material to the joint and surroundings. Aluminum rivets are light and can suit aluminum sheet, while steel options may provide greater strength. Stainless steel can help resist corrosion, but dissimilar metals may create galvanic corrosion in damp conditions. That detail is easy to miss. Compare the rivet’s stated material and mechanical properties with the applicable specification, not just its catalog name. For structural blind fasteners, ASTM F2280 may be relevant; confirm that its scope fits your application. Then check grip range against the combined sheet thickness. A rivet that is too short may not form correctly; one that is too long can leave a poor set. Test a sample in the actual materials, and inspect the formed head and joint before production. Specifications guide selection, but they do not replace fit checks.
| Rivet Type | Typical Use | Material Considerations | Applicable ISO or ASTM Specification | Selection Guidance |
|---|---|---|---|---|
| Open-end blind rivet, protruding head | General sheet-metal joining when access is available from one side only. | Common constructions include an aluminum-alloy body with a steel mandrel, or stainless-steel body and mandrel. Confirm the actual alloy and strength requirements for the selected product. | ISO 15977 — Blind rivets with break pull mandrel and protruding head, open end. ISO 14589 — Mechanical testing of blind rivets. | Choose a grip range that covers the total joined thickness. Consider head bearing area, joint loads, and corrosion compatibility between the rivet and joined materials. |
| Open-end blind rivet, countersunk head | Joints where a flush or low-profile surface is needed and the workpiece can accommodate a countersink. | Available in different body and mandrel materials; material choice affects strength, corrosion behavior, and suitability for the service environment. | ISO 15978 — Blind rivets with break pull mandrel and countersunk head, open end. ISO 14589 — Mechanical testing of blind rivets. | Check that the countersink depth and angle suit the fastener and sheet thickness. Avoid reducing the remaining material below the design requirement. |
| Open-end blind rivet, large flange head | Thin, soft, or relatively fragile sheet materials that benefit from a wider bearing surface. | Body and mandrel materials should be selected for the required load capacity and environmental resistance. Dissimilar metals may require corrosion review. | ISO 15979 — Blind rivets with break pull mandrel and large flange head, open end. ISO 14589 — Mechanical testing of blind rivets. | The larger head spreads load over a wider area, but does not by itself establish joint strength. Verify pull-out, shear, and substrate requirements for the application. |
| Closed-end blind rivet | One-sided installation where a closed tail is preferred to help limit liquid or particle entry through the rivet body. | Available in different body and mandrel materials. A closed-end rivet is not automatically a pressure-rated or leak-tight joint; sealing performance depends on the design and installation. | ISO 15980 — Protruding head, closed end; ISO 15981 — Countersunk head, closed end; ISO 15982 — Large flange head, closed end. ISO 14589 — Mechanical testing of blind rivets. | Select the head style to suit the surface and bearing needs. Specify any required sealing or pressure performance separately and validate it for the completed joint. |
| Steel structural rivet | Structural steel connections designed for riveted construction. | Use the steel grade and condition required by the structural design. Confirm that the rivet, connected parts, and corrosion-protection system are compatible. | ASTM A502 — Standard Specification for Steel Structural Rivets. | Use only where the connection design and applicable structural requirements permit rivets. Select grade and dimensions from the governing design documents and specification. |
| Aluminum-alloy rivet material | Rivet applications where low mass and aluminum-alloy properties are appropriate. | Alloy and temper influence strength, formability, and corrosion behavior. Consider galvanic interaction when aluminum is joined to dissimilar metals. | ASTM B316/B316M — Standard Specification for Aluminum and Aluminum-Alloy Rivet and Cold-Heading Wire and Rods. This covers specified material forms, not every finished-rivet design. | Verify the finished rivet’s dimensions and mechanical requirements separately. Match the alloy and temper to the forming process and service conditions. |
| Stainless-steel rivet material | Applications requiring stainless-steel material characteristics and corrosion resistance suited to the environment. | Stainless-steel grade matters; resistance varies with alloy, surface condition, exposure, and contact with other metals. | ASTM A493 — Standard Specification for Stainless Steel Wire and Wire Rods for Cold Heading and Cold Forging. This is a material-stock specification, not a complete finished-rivet specification. | Confirm the finished rivet’s grade, mechanical properties, and installation requirements. Assess crevice conditions and galvanic compatibility for the actual assembly. |
Specification note: Check the current edition of the cited standard and the product documentation before ordering. A material specification, rivet configuration standard, and joint-design requirement serve different purposes; none alone establishes suitability for every application.
Choosing among 3.2, 4.0, 4.8, and 6.4 mm rivets starts with the materials, not the tool drawer. A 3.2 mm rivet often suits light sheet metal, small brackets, or thin panels. A 4.0 mm size is common for general sheet-metal fastening. For thicker or more demanding joints, 4.8 mm may be appropriate, while 6.4 mm rivets are used for larger, heavier assemblies. These are starting points, not strength ratings.
Check the total material thickness against the rivet’s grip range. A rivet that is too short may not form a secure head; one that is too long can leave a loose or uneven joint. Match the hole diameter to the rivet specification, too. A hole that is visibly oversized can let the rivet shift, even when its nominal diameter seems right. I have found that measuring the stacked parts twice is less frustrating than enlarging a hole later.
Material compatibility and access also matter. For example, joining aluminum sheet to steel may need extra attention to corrosion risk and joint design. Confirm that your rivet-setting tool supports the chosen diameter, especially with 6.4 mm rivets, which need more setting force. Not diameter alone. If the joint carries vibration or substantial load, follow the fastener supplier’s technical data and test a sample assembly. I still sometimes focus too quickly on the diameter; grip range and hole quality deserve the same care.
How to Choose the Right Rivets for Your Project
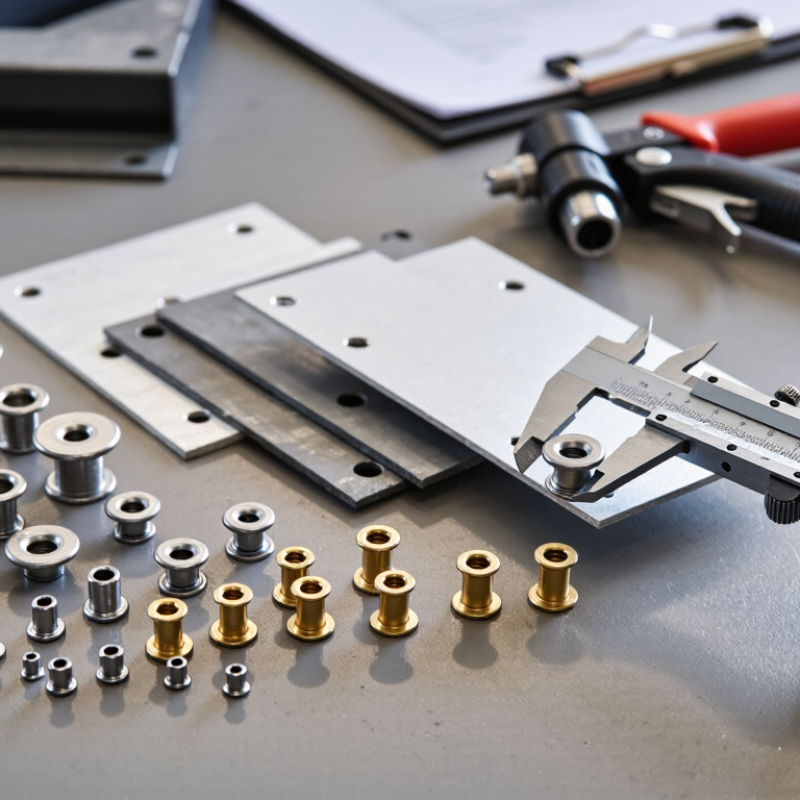
A rivet’s grip range is the total thickness it can securely clamp. Measure the joined materials together, rather than choosing a rivet by its overall length. For example, stack the two sheet-metal pieces and measure their combined thickness at the fastening point. Include coatings, washers, or a gasket if they will remain in the assembly. Small details matter. A compressed gasket may change the thickness more than expected.
Compare that measurement with the rivet’s stated grip range. The stack should fall within the range, not just near it. A rivet that is too short may not form a proper head behind the materials. One that is too long may set poorly or leave a loose joint. It is easy to overlook a folded edge or uneven surface, so measure more than one spot when the materials vary. A sample installation can reveal problems before you fasten the whole assembly. Slightly tedious, yes. But checking the set rivet for a firm hold and a flush head is more reliable than guessing from the package description.
Match the rivet’s grip range to the measured thickness of the joined materials.
The bars show example grip ranges; the dots show measured material-stack thicknesses. Choose a rivet whose grip range includes the full stack thickness. These examples are illustrative, not universal specifications—check the selected rivet’s datasheet before installation.
A reliable rivet joint begins with the hole, not the tool. Check the specified hole diameter and tolerance in the rivet manufacturer’s data; a hole that is too small can damage the rivet, while an oversized hole may leave it loose. I have caught myself reaching for a familiar drill bit without checking the sheet. That shortcut deserves a second look. Measure the finished hole, and remove burrs that could keep the rivet head from seating flat.
Edge distance matters just as much. Confirm how the manufacturer or project drawing defines it, then measure from the hole to the sheet edge consistently. Too little material around the hole can promote tearing, especially in thin sheet. Also match the rivet’s grip range to the combined thickness of the materials. Check that the installation tool, nosepiece, and setting capacity suit the rivet diameter and material. Use the tool as directed; excess force is not a fix for a mismatch. A small test joint can reveal a tilted head, loose setting, or distorted sheet before you fasten the full assembly. Not glamorous, but useful. If the test looks wrong, pause and recheck the data rather than guessing.